Welcome to the new ASW site. Some areas are still being updated, and we appreciate your understanding as we complete the rollout.
HERMETIC-Pumpen GmbH
Sealless Technology Unlimited
Global Leader in Sealed Pump Technology
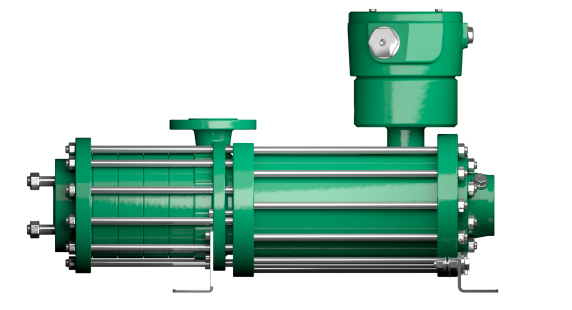
HERMETIC-Pumpen GmbH is a worldwide leading developer and manufacturer of hermetically sealed pump technologies. As specialists in canned motor pumps, the company has established itself globally with safe, reliable, and long-lasting pumps for the most extreme applications and hazardous media.
Their application range extends to fluid temperatures from -160°C to +480°C and system pressures up to 120 MPa. Combined with power ratings from 1 kW to 690 kW, they offer the largest range of canned motor pumps in the market.
Why Choose HERMETIC?
- Diverse application range
- Absolute leak-free operation
- Minimised life-cycle costs
- High reliability and availability
- Compact and simple installation
Global
Leader
Core Technologies
ZART Technology
Zero Axial and Radial Thrust - a quality characteristic for canned motor pumps ensuring extended service life and reliability
Extreme Temperature Range
Fluid temperatures from -160°C to +480°C for the most demanding industrial applications
High-Pressure Capability
System pressures up to 120 MPa with power range from 1 kW to 690 kW
Enhanced Safety
No mechanical seal improves operation safety, especially with dangerous or flammable media
Technical Specifications
Product Categories
Refrigeration Applications
Specialized pumps for CO2 and ammonia refrigeration systems
Features:
Applications:
Standard Applications
Versatile canned motor pumps for general industrial use
Features:
Applications:
Hot Applications
High-temperature pumps for thermal applications up to 480°C
Features:
Applications:
Low Temperature Applications
Specialised pumps for cryogenic applications with stable performance
Features:
Applications:
High Pressure Applications
Pumps designed for system pressures up to 120 MPa
Features:
Applications:
Vertical Design
Vertical configuration pumps for space-constrained installations
Features:
Applications:
Submerged Pumps
Hermetically sealed submerged pumps for tank and storage applications
Features:
Applications:
Magnetically Coupled Pumps
Advanced magnetic drive pump technology for hazardous liquids
Features:
Applications:
Vacuum Pumps and Systems
Liquid ring vacuum pumps and complete vacuum systems
Features:
Applications:
Industry Applications
Chemical and Petrochemical
Safe handling of aggressive chemicals, toxic media, and hazardous substances
Applications:
- Chemical processing
- Petrochemical industry
- Waste water treatment
- Sour water handling
Oil & Gas
Reliable pumping solutions for demanding oil and gas industry applications
Applications:
- Upstream operations
- Refining processes
- Pipeline applications
- Offshore platforms
Refrigeration
Specialized pumps for CO2 and ammonia refrigeration with 50+ years of experience
Applications:
- CO2 refrigeration
- Ammonia systems
- Industrial cooling
- Cold storage
Railway
Glycol pumps for railway industry applications meeting specific standards and regulations
Applications:
- Railway glycol systems
- Engine cooling
- Railway industry standards
Energy
Pump solutions for renewable energy and power plant applications
Applications:
- Renewable energy
- Power plants
- Energy systems
- CCUS applications
Ready to Explore HERMETIC Solutions?
Contact our team to discuss your specific requirements and find the perfect HERMETIC pump solution for your application. We provide comprehensive support throughout the entire lifecycle of your equipment.
Get in Touch