Welcome to the new ASW site. Some areas are still being updated, and we appreciate your understanding as we complete the rollout.
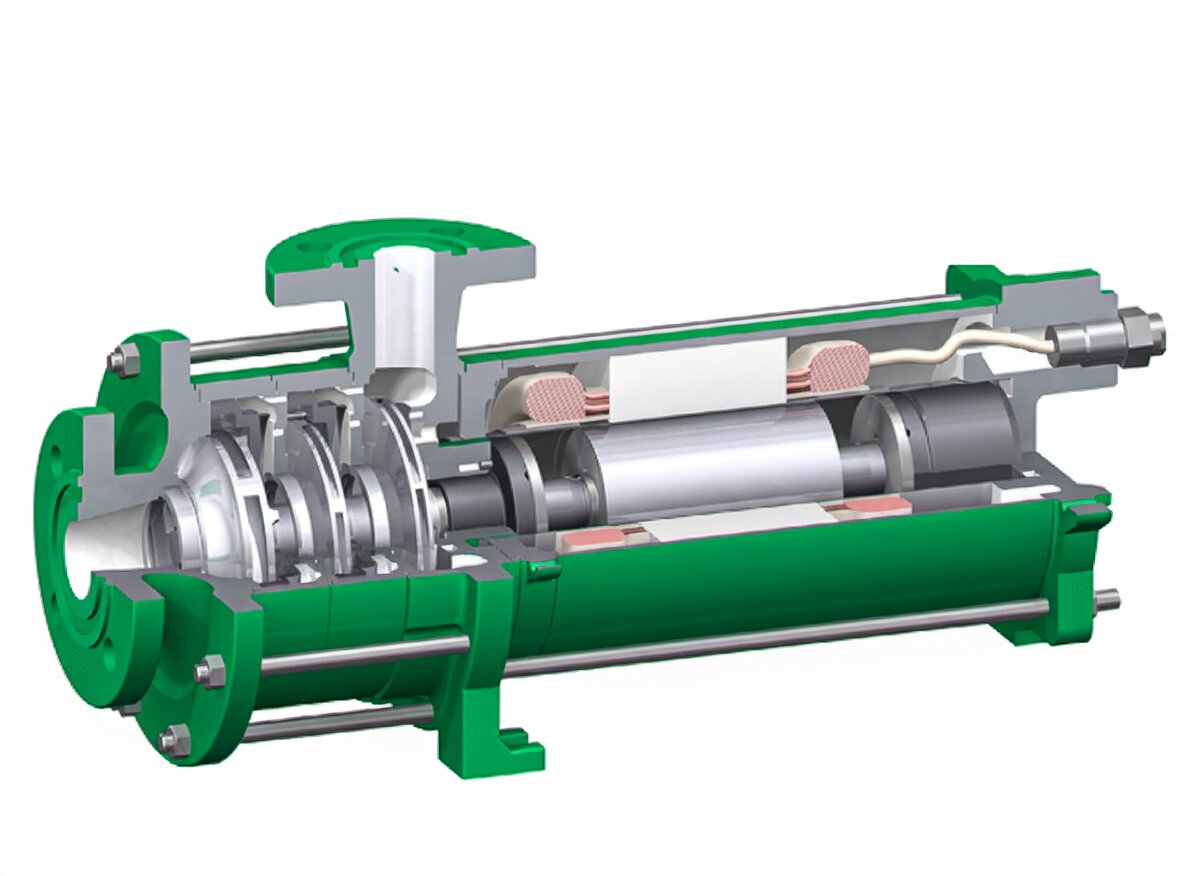
Canned Motor Pumps
Your Trusted Partner for Canned Motor Pump Solutions
Excellence in Canned Motor Pump Technology
ASW is a premier supplier and exclusive agent for top-tier international canned motor pump manufacturers. We specialize in delivering highly efficient solutions to meet your fluid transfer requirements, no matter where they are needed.
Our extensive product selection ensures that we can provide reliable, cost-effective solutions across a wide range of industries. We focus on delivering tailored options that meet both your technical and budgetary needs.
Comprehensive Support
- Comprehensive site evaluation and specific product selection
- Custom designs for all applications
- Routine maintenance and repairs performed
Premium
German Engineering
Our Brand Partner

Hermetic Pumpen
HERMETIC-Pumpen GmbH is a leading developer and manufacturer of hermetically sealed pumps. As specialists for canned motor pumps, they have earned a global reputation for enduring pumps used in the most extreme applications.
Key Features:
Applications:
Product Categories
Centrifugal Canned Motor Pumps
Pumps for refineries and petrochemical applications.
Features:
Applications:
Extreme Temperature Pumps
Specialised pumps designed for EXTREME temperature applications.
Features:
Applications:
Environmental and Health Hazard Media
Pumps engineered aggressive and toxic fluid handling.
Features:
Applications:
Refrigeration Pumps
Specialized pumps for refrigeration and cooling systems
Features:
Applications:
The Critical Importance of Zero-Leakage Technology
In today's industrial environment, the risk of leaks and environmental contamination from pump failures is a serious concern. Canned motor pumps provide the ultimate solution for handling hazardous, toxic, or environmentally sensitive fluids safely and reliably. When dealing with aggressive chemicals, volatile compounds, or temperature-sensitive applications, traditional sealed pumps simply cannot match the safety and performance of canned motor technology.
For this reason, canned motor pumps are essential in critical industrial applications! The operational safety, environmental protection, and maintenance cost savings you gain by eliminating leakage risks far outweigh the investment in premium canned motor pump technology. When failure is not an option, canned motor pumps deliver the zero-leakage performance your operations demand.
Ready to Enhance Your Pumping Systems?
Contact our team of experts for personalized advice and solutions tailored to your specific canned motor pump requirements.
Get in Touch